How to Source Stamped Contact Spring for Global Buyers?
Sourcing a Stamped Contact Spring for global production requires more than comparing unit prices. Buyers must connect electrical performance, forming accuracy, material quality, and supply reliability. A spring may look simple in a sample tray, yet its contact force can change after plating, repeated compression, or shipment across humid climates. Small details matter. So does traceability.
Dr. William C. Brown, a contact-spring design specialist, states, “A reliable contact spring begins with a controlled design, not a hopeful inspection.” This principle should guide supplier evaluation. Request material certificates, dimensional reports, plating specifications, tooling details, and force-deflection data. Confirm whether the supplier controls stamping, deburring, heat treatment, and surface finishing internally. Ask for production samples from the actual tool. Laboratory prototypes can hide production weaknesses.
Global buyers should also examine communication habits. Can the manufacturer explain tolerance limits clearly? Can it provide a corrective-action report when results drift? Can it protect drawings and manage engineering changes responsibly? These questions reveal practical maturity. Certifications help, but certificates alone cannot prove stable output. That is an uncomfortable truth.
A careful sourcing process includes trial orders, inspection plans, packaging tests, and realistic lead-time reviews. Consider customs documentation and regional service support. Do not accept vague claims such as “premium quality.” Ask for measurable evidence. I have seen supplier comparisons become too focused on price, while tooling maintenance receives little attention. That approach may reduce the first invoice and increase later disruptions. The best decision is not always the cheapest one. It is the option that keeps contact force, conductivity, and delivery performance dependable over time.
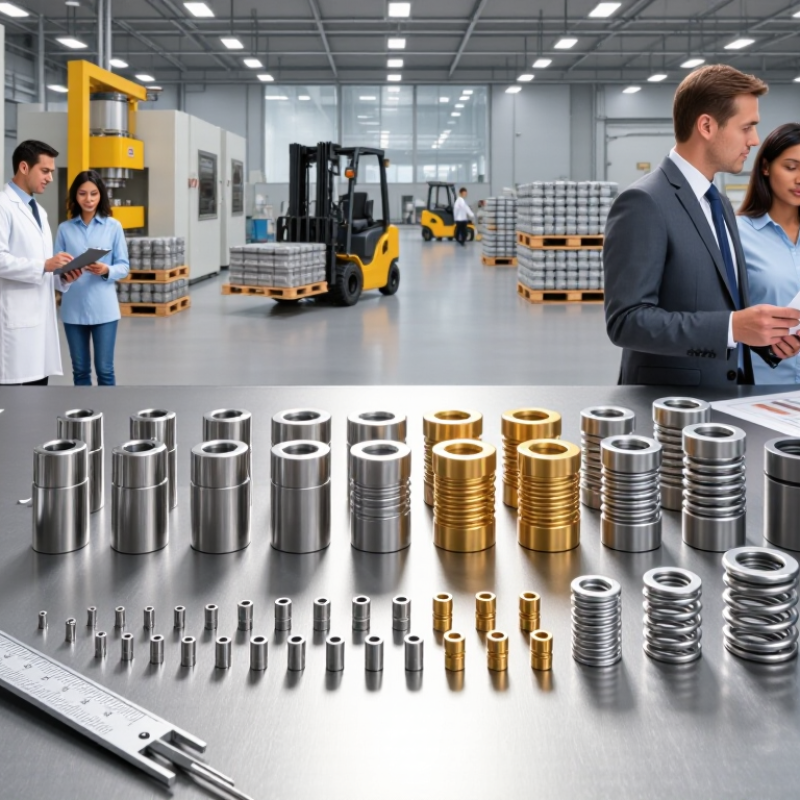
Define the Performance Requirements of a Stamped Contact Spring
A stamped contact spring should be specified by performance, not appearance alone. During supplier reviews, I define its current rating, contact force, travel, and operating temperature. These values reveal whether the spring suits a connector, sensor, or compact switching assembly. The required force must remain stable after repeated compression. A beautiful part can still fail electrically.
Measure contact resistance at the intended current and after cycling. Specify the maximum resistance increase allowed. State the working deflection, overload limit, and minimum service life. For harsh environments, include humidity, vibration, salt exposure, and temperature changes. Material choice matters, but coating thickness and adhesion matter too. Use a controlled drawing with tolerances for width, thickness, bend angle, and contact height.
Tips: Request sample testing before mass production. Review force-deflection curves, resistance data, and dimensional reports. Ask how testing reflects real assembly conditions. Confirm inspection equipment and sampling frequency. Do not accept “standard performance” without numbers.
I once treated contact force as the main requirement. That was incomplete. Spring relaxation and mounting variation later became concerns. Now I connect every requirement to a test method and acceptance limit. Suppliers should provide traceable records for each production batch. A small tolerance can change alignment. A minor burr can damage a mating surface. Prototype parts should be checked with the actual housing, not only with laboratory fixtures. The specification may need revision after testing, and that is normal. Good sourcing begins with measurable performance and honest technical discussion.
Identify Suitable Materials, Plating Options, and Spring Geometries
How to Source Stamped Contact Spring for Global Buyers?
Identify Suitable Materials, Plating Options, and Spring Geometries
Sourcing a stamped contact spring starts with the mating environment, not the catalogue. Phosphor bronze suits cost-sensitive connectors and offers stable fatigue performance. Beryllium copper provides higher conductivity and stronger spring retention. Stainless steel works better where corrosion resistance matters more than conductivity.
Choose plating after reviewing current, humidity, temperature, and mating cycles. Tin is practical for many power contacts, but it may develop fretting concerns. Nickel improves barrier protection and wear resistance. Gold supports low-level signals and repeated mating, although its cost can rise sharply.
The International Energy Agency reported that global electric-car sales exceeded 17 million in 2024. This growth increases demand for compact, reliable electrical interfaces. Yet, automotive sourcing often reveals an uncomfortable truth: a good material can still fail when the geometry is poorly controlled.
Spring geometry needs equal attention. Cantilever, U-shaped, and dual-beam designs provide different normal forces and deflection ranges. Ask suppliers for force-versus-deflection curves, burr limits, flatness data, and salt-spray results. ASTM and IEC test methods can improve comparison, but test conditions must match actual use.
Tips: Request three samples with different beam lengths. Measure contact force at the working height. Check plating thickness after forming, not only before stamping. A small radius error can change performance. Do not trust appearance alone. Review the supplier’s capability studies, traceability records, and corrective-action history. I would also repeat the test after aging, because fresh samples can hide long-term weakness.
Evaluate Manufacturers by Tooling, Quality, and Production Capabilities
How to Source Stamped Contact Spring for Global Buyers?
When sourcing a stamped contact spring, examine the manufacturer’s tooling before reviewing the quoted price. Tooling matters. Ask whether the supplier designs progressive dies internally or outsources them. Inspect die drawings, material selection, expected tool life, and maintenance records. A reliable maker should explain replacement plans for worn punches and forming inserts. Request a small pilot run. It can reveal burrs, uneven forming, and unstable spring force before mass production begins.
Quality control must cover more than visual inspection. Confirm dimensional tolerances with calibrated gauges and verify spring force at the required working height. Ask for material certificates, surface-finish records, and fatigue-test data. Process capability reports, such as Cpk results, can show whether production remains stable. I would also check how operators separate defective parts. Mixed lots create expensive problems. A polished sample can hide weak controls.
Production capability deserves equal attention. Review press tonnage, strip-width limits, automation, inspection frequency, and monthly capacity. Ask for batch traceability from raw material to final packing. Backup equipment is useful when a critical press stops unexpectedly. During supplier audits, compare stated capacity with actual machine loading. No audit is perfect. I once underestimated maintenance delays because the supplier shared only ideal lead times. Leave room for tooling repairs, engineering changes, and transport interruptions. Clear approval records and realistic production schedules support dependable global sourcing.
Verify Samples, Testing Results, and Compliance Documentation
How to Source Stamped Contact Spring for Global Buyers?
A stamped contact spring may look simple, but small dimensional errors can reduce contact force. I recommend checking samples against the approved drawing and a physical golden sample. Measure free height, wire thickness, pitch, and spring load at defined deflections. Request load-deflection curves, fatigue-cycle results, and electrical resistance data. Test plating thickness and corrosion resistance, especially when springs face humidity or salt exposure. A certificate alone is not enough.
Ask for reports issued by an ISO/IEC 17025-accredited laboratory. This improves traceability, although it does not remove every risk. The test report should identify the exact material grade, lot number, equipment, test method, and acceptance limits. Supplier quality records should also include first-article inspection and change-control procedures. Reports using only “passed” need deeper review.
Compliance files require equal attention. RoHS restricts ten substances, while the European Chemicals Agency’s Candidate List contained more than 240 substances in 2024. Request current RoHS and REACH declarations, material composition data, and a Certificate of Conformity. ISO 9001 certification can support process control, but it does not prove product performance. I have seen strong paperwork paired with inconsistent batches. Retain samples from each production lot, and repeat critical tests after tooling or plating changes. Some sourcing teams skip this step. That is where avoidable failures begin.
How to Source Stamped Contact Spring for Global Buyers?
Verify samples, testing results, and compliance documentation before approving a supplier.
How to use this checklist: Request stamped contact spring samples that match the approved drawing, review dimensional and functional test results, and confirm that the supplier’s compliance file references the requirements applicable to the destination market.
The chart shows the official publication or adoption year associated with four commonly reviewed references: REACH Regulation (EC) No 1907/2006, RoHS Directive 2011/65/EU, ISO 9001:2015, and IATF 16949:2016. These years identify the governing reference, not a supplier performance score.


